Quick answer
EHL BIO prioritizes safety by conducting rigorous quality control on every cell lot within our GMP-certified facilities, capable of producing 6,000 lots annually. Our processes include Class 100 cleanroom monitoring and thorough purity testing before clinical application.
Key takeaways
- Produced under international GMP standards with a capacity of 6,000 lots per year.
- Utilizing Class 100 Clean Rooms for maximum contamination prevention.
- Comprehensive testing covering cell purity, viability, and potency.
- Cell preservation using liquid nitrogen systems at -196°C to maintain quality.
The Significance of GMP Standards in Cell Production
Good Manufacturing Practices (GMP) represent the core philosophy that EHL BIO strictly follows in isolating and culturing stem and immune cells. We are approved by the Ministry of Food and Drug Safety (MFDS) and were the first in Korea to be licensed as a Human Cell Management Business under the Advanced Regenerative Medicine and Advanced Biopharmaceuticals Act.
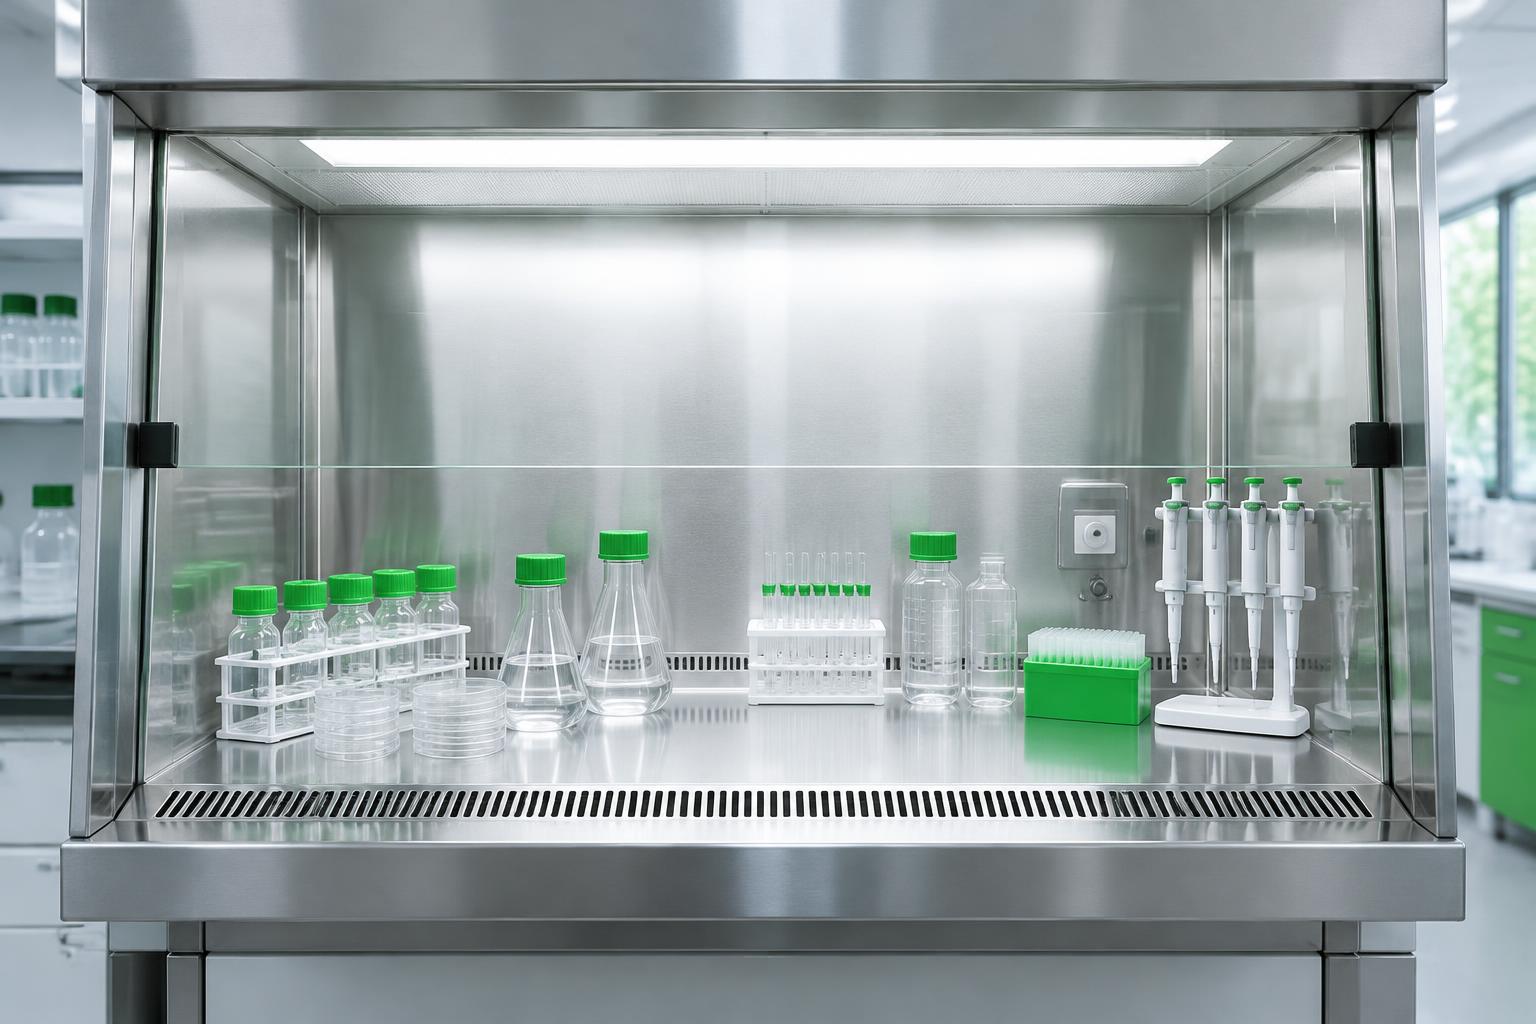
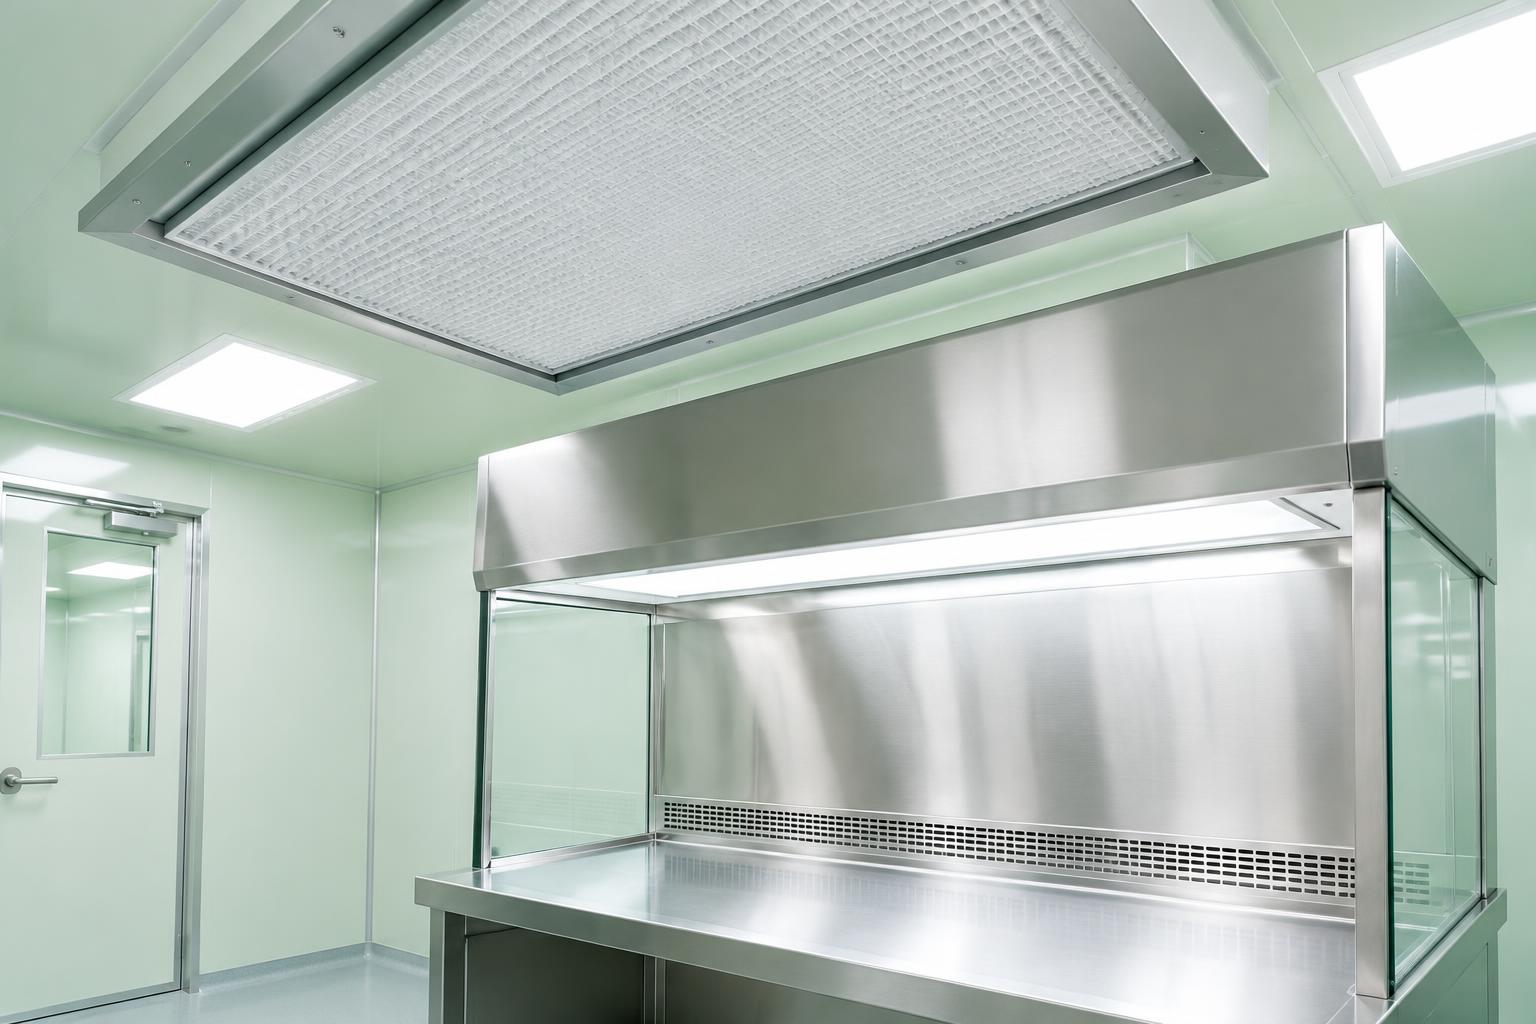
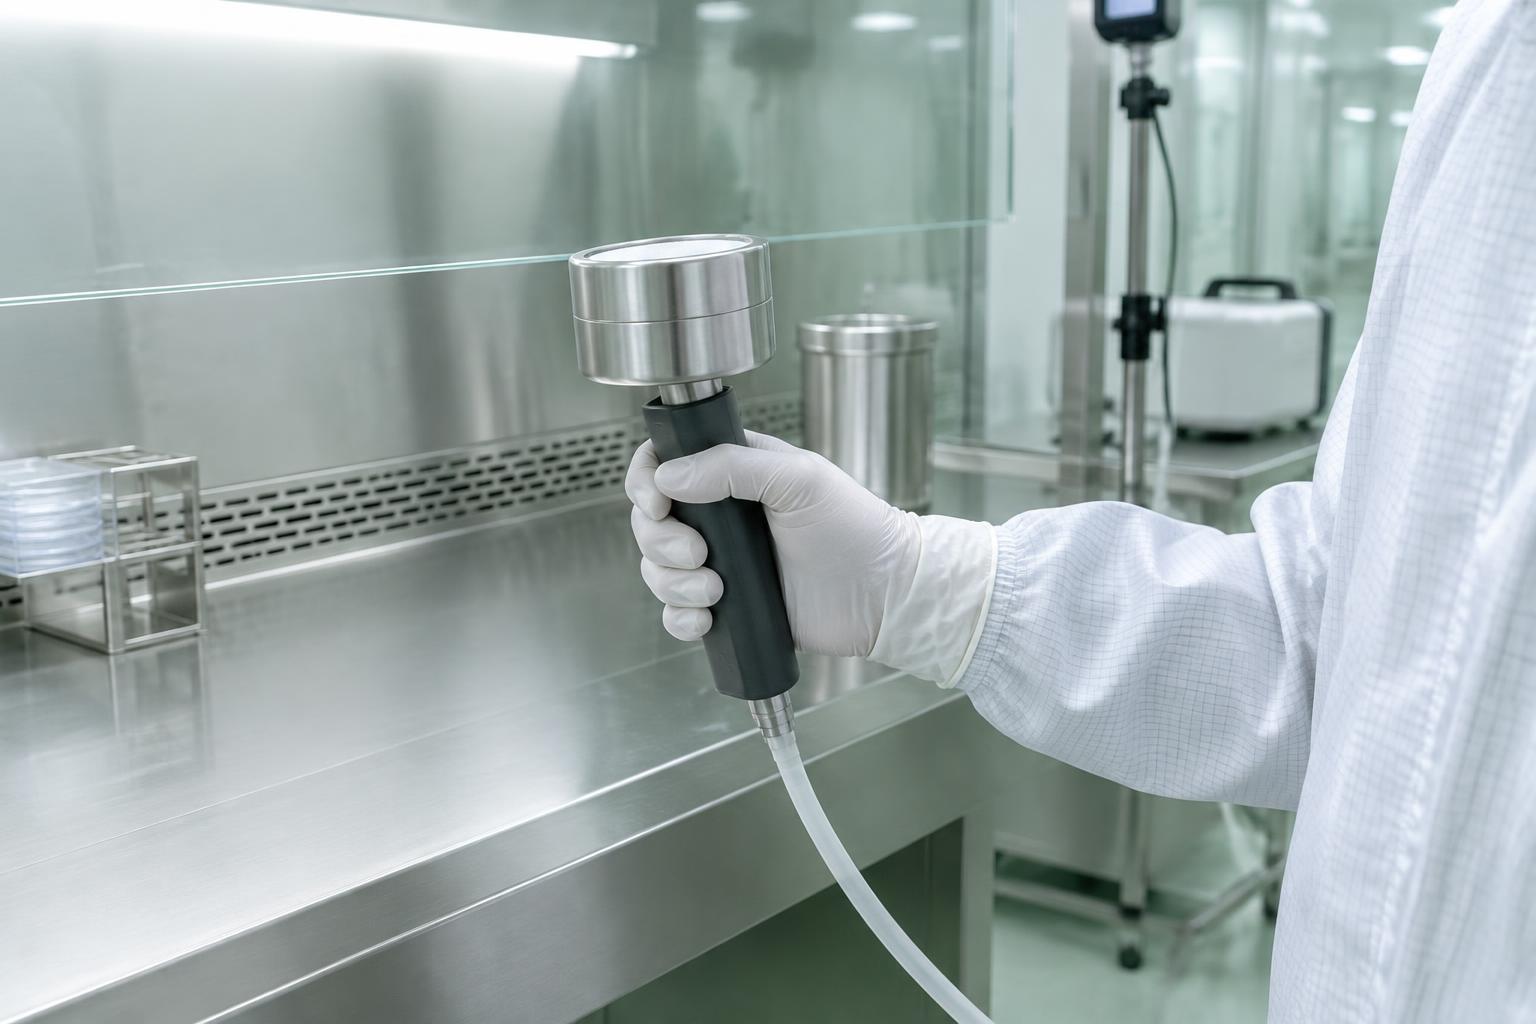
Our production system is designed to maintain consistent quality standards. Our GMP facilities are equipped with advanced technologies, including Biological Safety Cabinets (BSC) and AHU air management systems with HEPA filters, ensuring that every step is contamination-free and safe according to EHL team assessments for all patients.
Class 100 Cleanrooms and Environmental Control
At EHL BIO, we utilize Class 100 cleanrooms, a high-level standard that minimizes airborne particles to ensure a pristine environment for cell culture. Our team of over 85 researchers operates under strict protocols to achieve cell yields up to 1,000 times higher than average standards.
Beyond cleanliness, we employ liquid nitrogen storage technology for cryopreservation at -196°C. This maintains the cell's youthfulness and potency as if they were freshly harvested, ensuring that each session aims for restoration and quality of life according to the medical team's care plan.
Class 100 safety standards and rigorous quality checks for every lot are EHL BIO's promise for the best restoration and quality of life goals.
Comprehensive Quality Check for Every Lot
Every cell lot cultured at the EHL BIO research center undergoes detailed quality testing before clinical use. This includes assessing Cell Viability, Purity, and Potency to ensure the cells possess an effective Homing Effect for targeted care of worn tissues.
We conduct biological safety checks to confirm the absence of infections or foreign materials, aligning with stringent cell processing center standards. This meticulousness ensures that patients receive high-quality cell therapy products that support a good quality of life.
Innovation and Reliable Certifications
EHL BIO's success in quality control is evidenced by numerous patents, such as our SVF isolation kits and high-purity urine-derived stem cell (UDSC) culture methods, which earned the IR52 Jang Young-shil Technology Innovation Award in 2025. These accolades reflect our commitment to setting new standards in regenerative medicine.
We prioritize not only technology but also accessible service for Thai patients. EHL Thailand provides a dedicated Thai-speaking coordination team to support patients from the initial consultation until post-treatment follow-up after returning from Korea, ensuring that improved quality of life is an achievable goal for everyone.
Frequently asked questions
What does EHL BIO test for in each cell lot?
We test for cell purity, viability, potency, and biological safety to ensure no contamination before any clinical application.
Why is a Class 100 laboratory important?
It is a high-level cleanroom standard that prevents dust and microbial contamination during the cell culture process, ensuring patient safety according to EHL team assessments.
What are the goals for restoration and quality of life when using long-term stored cells?
We use cryopreservation technology in liquid nitrogen at -196°C, which maintains cell integrity and quality over long periods to effectively support restoration goals.
Related conditions
Based on EHL BIO information: EHL BIO · EHL BIO · EHL BIO · EHL BIO. Each care plan follows an individual EHL assessment.